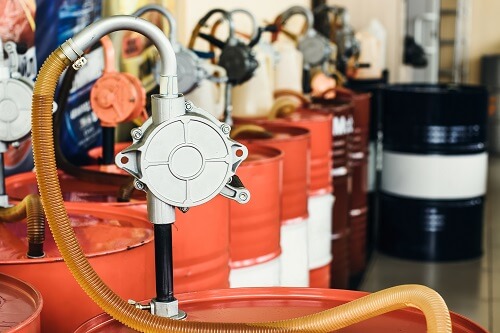
Structure and Design of Drum Pumps
Whether manual operation suffices or you and your staff require an electric drum pump depends on the operating environment and the medium stored inside the drum. Manual and electric variants differ substantially in operational complexity and suitability. Electric pumps work faster and streamline daily operations when multiple drums need emptying in short succession. Manual hand pumps, by contrast, are considerably more cost-effective and purpose-built for occasional transfer tasks.
Both designs feature a pump tube assembly along with a discharge hose or rigid dispensing pipe. On manual drum pumps, the pump mechanism and suction tube are actuated via a hand lever operated by the user. Electric pumps connect directly to mains power and initiate pumping at the touch of a button thanks to an integrated motor.
The drum pumps in our range are tailored for compatibility with diverse drum styles, matching specific volumes and contents. Suction tube diameters generally measure between 32 and 41 mm. Immersion tube lengths reach up to 1 meter and, on many of our models, adjust flexibly via telescopic suction tubes. You can adjust the length between 400 and 900 mm to meet specific requirements, whether extracting liquids from CurTec wide-neck drums or standard removable-head drums.
Manual Drum Pumps
Alongside specialized acid drum pumps, our assortment includes drum pumps for water and dedicated oil drum pumps. The latter is equally suited for diesel and alcohols, fabricated from polypropylene (PP) for elevated structural durability and temperature resistance. Petrol drum pumps incorporate specialized NBR seals engineered for mineral oil derivatives, combined with a tool-steel drive shaft. Component specifications like sealing materials are manufactured to precise industry standards based on the pumped fluid. Hand-lever oil pumps can be configured to deliver 0.3 to 0.45 liters per stroke, providing ample delivery capacity for small-to-medium drum volumes in low frequencies.
When operating drum pumps manually, precautions must be observed due to the operator's physical proximity to the chemical. Component parts for flammable liquid pumps are fabricated from stainless steel to maximize operational safety. In addition to hazardous materials, our manual drum pumps handle water and low-viscosity food liquids such as milk.
Hand pumps for sensitive media:
-
JP-07-1 for mineral oils (NBR seals), blue
-
JP-07-2 for alkaline media (EPDM seals), red
-
JP-07-3 for mild acids (FKM seals), green
We supply dedicated, color-coded drum pumps matching acids, alkaline fluids, and mineral oils for clear visual differentiation. For instance, pumps designated for alkaline solutions feature seals made of ethylene propylene diene monomer rubber (EPDM). Even 200-liter barrels can be emptied rapidly, dispensing into 20-liter canisters within approximately one minute. All three pump models operate reliably up to 40 °C and allow fast, straightforward cleaning.
Electric Drum Pumps
Electric drum pumps are engineered for larger-scale industrial throughput and save operations significant labor time. Our selection features configurations for common chemical reagents widely used across food production, medical, and pharmaceutical sectors. Manufactured from PP and driven by a 230 V motor, these pump units deliver flow rates up to 93 l/min.
These compact electric drum pumps provide high mechanical durability, proving ideal for low- to medium-viscosity fluids. Compatible media may range from neutral to corrosive, provided they are non-flammable. The units adhere to IP 24 protection standards and Class II electrical insulation, ensuring splash-proof containment and double insulation. Power connection is handled via a 5-meter power cable fitted with a standard Schuko plug.
Drum pumps for highly aggressive media are manufactured from polyvinylidene fluoride (PVDF) under equivalent protective classifications. Complete sets include a 2-meter multi-purpose hose, stainless steel hose clamps, and a chemical nozzle. For petroleum and mineral oil products, aluminum drum pumps are available, capable of delivering discharge rates up to 112 l/min via an axial rotor.
An alternate impelling geometry is available across pump categories. Axial rotors operate efficiently at standard delivery heads and normal pressure. When higher delivery heads must be overcome, radial impellers can be installed to handle steeper vertical lift at reduced flow rates.